Quick Answer: Cosmetic GMP means good manufacturing practice: the people, premises, procedures and records used to make cosmetic products consistently under controlled conditions. It connects raw-material approval, hygiene, production, testing, release and traceability. A certificate can support supplier assessment, but everyday compliance depends on actual operations and evidence, and a GMP certificate does not provide universal market approval.
Understand GMP as a working manufacturing system
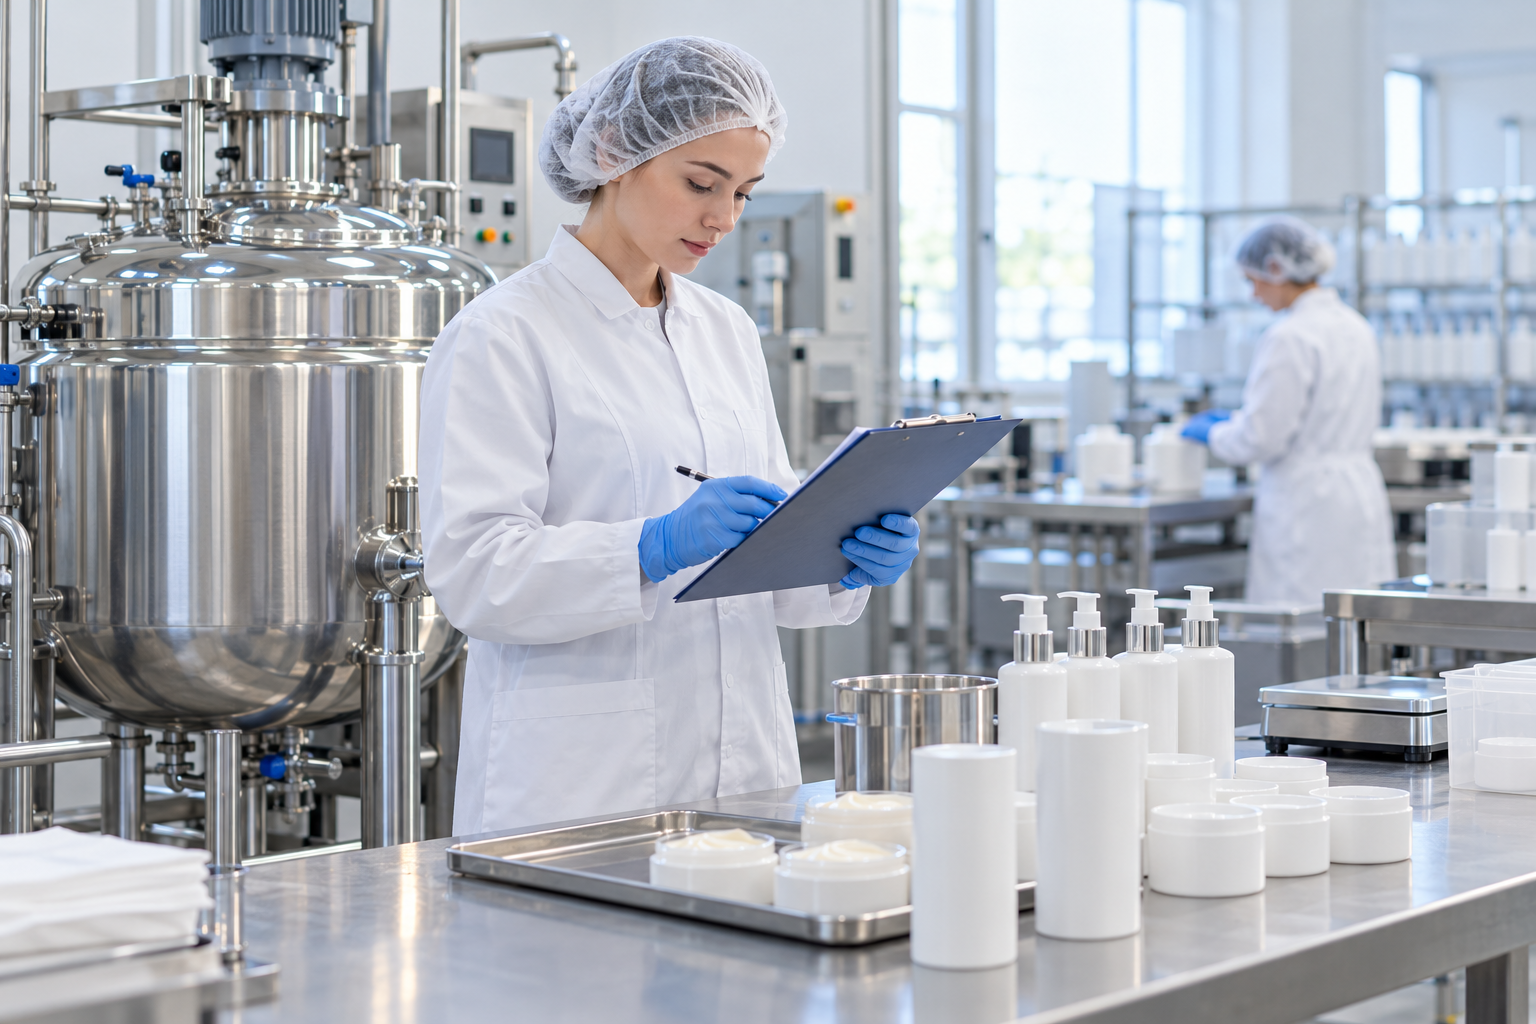
A cosmetic formula describes what a product should contain. GMP controls how the factory repeatedly turns that formula into acceptable batches. It helps a team avoid preventable mix-ups, contamination and undocumented changes, then identify and investigate problems when they occur. A clean-looking room alone cannot demonstrate all of these controls.
The BSI ISO 22716 scope summary describes guidelines covering production, control, storage and shipment of cosmetics. Its published scope also identifies exclusions, including research and development and finished-product distribution. A brand should therefore identify the operations it needs assessed rather than assuming that a manufacturing standard covers every activity from concept to retail.
The practical question is whether an operator can explain what to do, find the current instruction, perform the task and leave a reliable record. Ask for a recent batch example rather than only a policy manual. The documents should connect the materials received, the equipment used, the process performed and the decision to release the goods.
| Control area | Everyday practice | Evidence to request |
|---|---|---|
| People and hygiene | Train staff for assigned work and hygienic entry | Training records and observed practices |
| Materials and equipment | Approve status before use and prevent mix-ups | Receipt, cleaning and equipment-status records |
| Production and quality | Follow controlled instructions and review results | Batch record, specifications and release decision |
| Traceability and improvement | Investigate deviations and locate affected stock | Investigation, actions and distribution records |
Begin with people, premises and material flow
Define responsibilities before scaling production. The person weighing a material, the person checking it and the person authorising release need clear duties and escalation routes. Training should address the actual task, including how to respond to an unexpected reading or a missing label. A signature confirming attendance is useful only when the operator can apply the instruction.
Walk the route taken by incoming ingredients, packaging, bulk product and finished goods. Check how the factory distinguishes approved, quarantined and rejected stock. Separation may involve designated areas, controlled systems and visible identification suited to the site. The important outcome is that an operator cannot accidentally select a rejected drum because it resembles an approved one.
Use the FDA cosmetic GMP inspection checklist as an official self-inspection reference. It discusses facilities, equipment, materials and production controls. Treat its recommendations as a source for reviewing operations; do not describe the checklist as a certificate issued to a supplier. A supplier’s practices still need assessment against the applicable requirements and agreed standard.
Control ingredients, water and packaging before production
Create acceptance specifications that fit each material and its intended function. Reconcile the supplier name, material identity, lot number and received quantity. Define the checks needed before use and record the decision. Supplier paperwork can support the assessment, but an attractive certificate of analysis should not replace a reasoned incoming-control programme.
Water used in a formula or cleaning process deserves a defined quality and monitoring plan appropriate to its use. A factory should know the sampling points, test approach, action levels and response to an unacceptable result. Trending helps reveal deterioration that a single isolated passing result may miss. Specific limits should be justified for the operation instead of copied without context.
Packaging can also create errors. Similar bottles and cartons need clear identity controls, and closure or pump changes may affect performance. Coordinate the approved pack specification with the formula and filling process. The brand should tell the manufacturer about artwork revisions, destination-market changes and any new instructions that affect the production run.
| Decision | Manufacturer responsibility | Brand contribution |
|---|---|---|
| Manufacturing method | Control equipment, instructions and execution | Confirm product brief and approved formula |
| Pack and claims | Check supplied specifications and line identity | Approve artwork and market-specific claims |
| Release evidence | Review batch results and deviations | Agree information needed before shipment |
| Change and complaint | Investigate manufacturing impact | Supply market feedback and approve agreed changes |
Make the batch record tell a complete story
An effective record links a batch to the exact formula and instruction revision used. It identifies material lots, relevant equipment, processing stages, in-process observations and accountable operators. Record results when work occurs. Reconstructing an entire shift from memory at the end weakens the evidence and can hide the point where a problem started.
Consider a moisturiser that becomes thinner than expected. The investigator needs more than a final viscosity value. Useful evidence can include the ingredient lot, weighing checks, process sequence, temperatures, mixing conditions, hold period and the method used for the measurement. These are examples of information to select for the process, not universal numeric settings for every cream.
When work differs from the instruction, record the deviation and assess the affected material. Do not make an unapproved adjustment merely to obtain a passing result. The quality review should explain the decision, any additional checks and whether the batch can be released, reworked under an authorised method or rejected. Preserve the original observations alongside the conclusion.
Keep cleaning, quality control and release connected
A cleaning procedure needs to suit the equipment, residue and next operation. Define who performs it, the materials used, the checks needed and the status identification after completion. Shared utensils and transfer hoses deserve attention because they can cross otherwise well-separated areas. Schedule maintenance so damaged surfaces or leaking components do not become recurring quality risks.
Finished-product checks should follow an approved specification and suitable methods. Product type and risk determine the testing programme; GMP does not mean that one generic test panel proves every cosmetic safe. Stability, preservation and packaging compatibility also need appropriate product-development and safety evidence beyond routine batch measurements.
Release is a documented decision by authorised personnel after the required information is reviewed. Agree how the brand receives the relevant results and how holds are communicated. A shipping deadline should not silently become an acceptance criterion. If information remains incomplete, identify the outstanding item and maintain the agreed status control until it is resolved.
| Item | What it helps demonstrate | What it does not establish alone |
|---|---|---|
| GMP operating records | How specific work was controlled | All destination-market requirements |
| Batch certificate of analysis | Reported results for the identified batch | The entire factory quality system |
| Third-party GMP certificate | Assessment within a stated scope | Universal product approval or permanent compliance |
| Product safety assessment | Safety reasoning for the assessed product | Correct execution of every future batch |
Use traceability and corrective action to learn from problems
Choose a finished batch and work backwards to materials, process records and release. Then work forwards to shipments. This exercise reveals gaps between production coding and commercial records. Agree how quickly both parties can identify potentially affected goods and who makes decisions when information is incomplete.
Complaints should be reviewed for patterns, including repeated leakage, unexpected odour or changes in appearance. Retain enough information to distinguish a manufacturing issue from storage, handling or packaging damage. An investigation should define the cause as far as the evidence supports, implement corrective action and check whether that action worked in later production.
For an outsourced project, discuss these controls with the OEM/ODM cosmetics manufacturer before the order is placed. A quality agreement can define document access, change notification and complaint cooperation. Commercial confidentiality can be protected through controlled access while still allowing a competent reviewer to assess the evidence.
Separate GMP compliance from certification and market access
GMP obligations and certification arrangements depend on the destination and the relevant framework. In the EU, European Commission cosmetics harmonised-standards overview requires manufacturing to follow GMP and provides a presumption of compliance when manufacture follows relevant harmonised standards whose references are published in the Official Journal. That provision is not a universal requirement to purchase a third-party certificate.
ISO explains its role in standards and certification. External bodies conduct certification. Ask which standard, legal entity, site and activities are covered, and verify current status with the issuer. A certificate for another address or a narrower operation may not cover the production you intend to buy.
Keep the destination review separate. Formula restrictions, safety assessment, labeling, notifications and local operator responsibilities still need attention. The Korean cosmetic regulations guide illustrates why a manufacturing quality system and local market obligations need coordinated review. For a supplier discussion, contact the project team with the product type, manufacturing route and intended markets so the evidence request can match the project.
| Framework | GMP evidence focus | Separate review |
|---|---|---|
| European Union | Article 8 GMP and relevant harmonised standards | Safety assessment, information file and responsible person |
| United States | Controlled operations and relevant FDA inspection guidance | Current product, facility and labeling obligations |
| Other destinations | Applicable local manufacturing framework | Classification, local operator and market entry requirements |
Frequently asked questions
What does GMP stand for in cosmetics?
Good manufacturing practice. It describes controls for consistent cosmetic manufacture, including personnel, premises, materials, production, quality review and records.
Is GMP the same as product testing?
No. Testing provides selected results, while GMP also controls how materials and products are handled, made, identified, investigated and released.
Does a GMP certificate approve every product?
No. A certificate has a defined issuer and scope. Product safety, claims and destination-market requirements still need their own assessment.
Can a brand outsource GMP responsibility?
A manufacturer controls its operations, but the brand still needs suitable supplier oversight and to fulfil its own legal and contractual responsibilities. Define the handoff clearly.
What is a useful first supplier check?
Trace one recent batch from approved material lots through manufacturing and release to shipment, then compare the records with the site and activities being offered.
Last reviewed: 28 October 2026. General manufacturing and supplier-review information, not product-specific legal, certification or safety advice. Confirm current requirements and the relevant certification scheme with qualified advisers for each destination market.